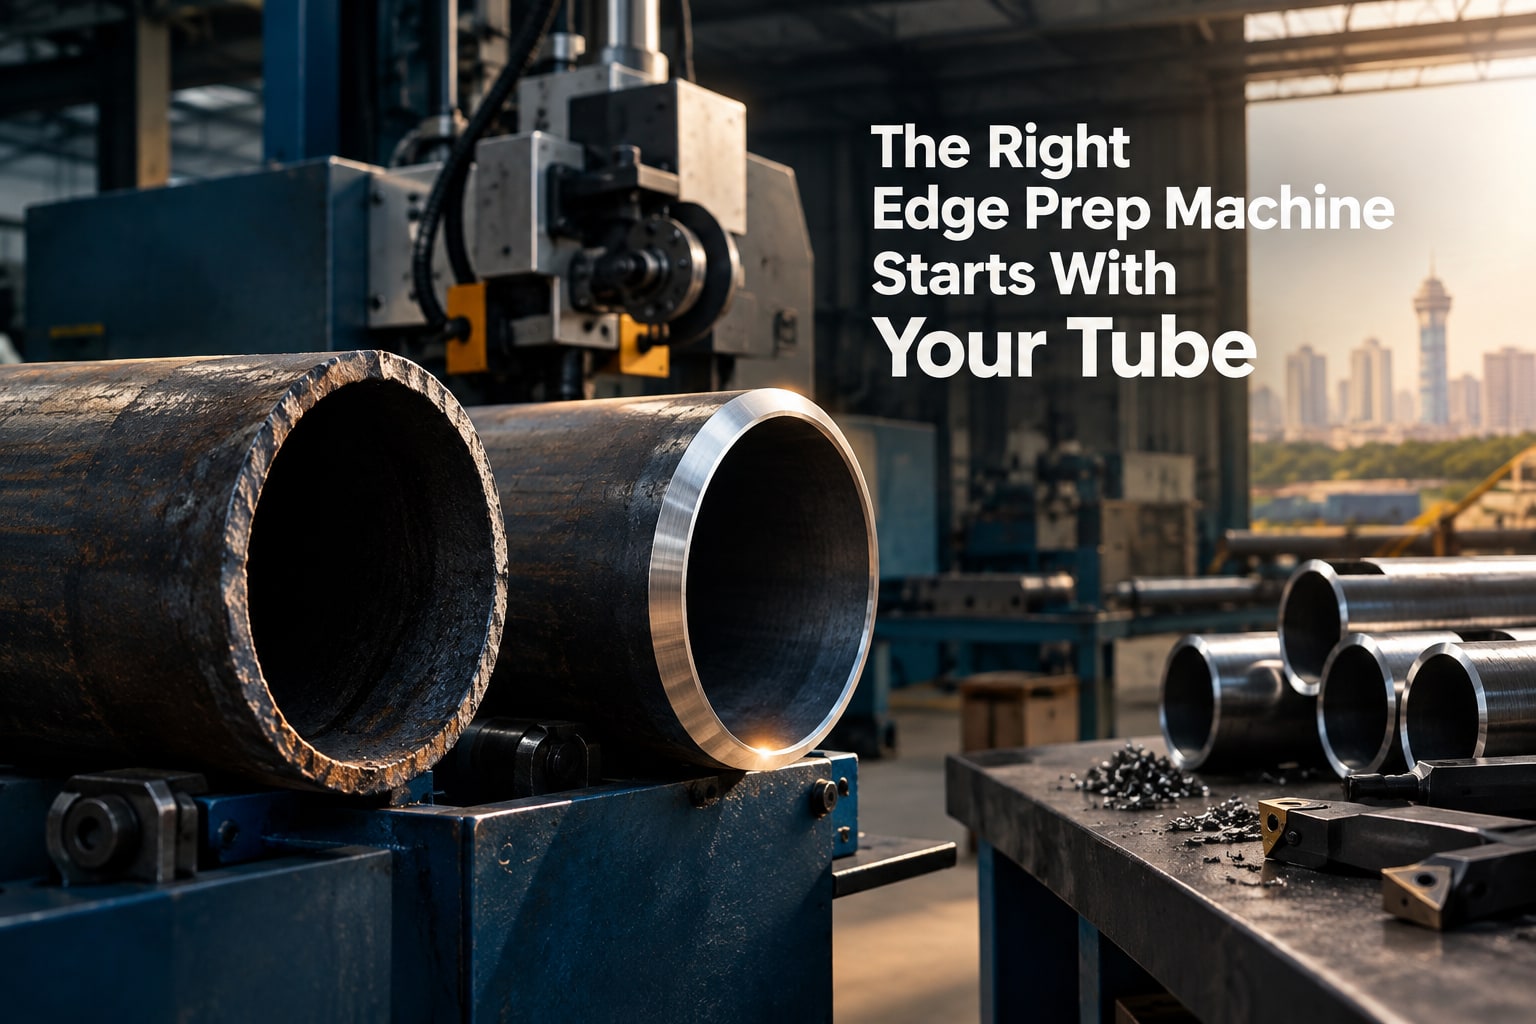
A machine listed as an edge preparation machine may be a stationary pipe beveler, portable OD-mounted unit, tube end facer or combined facing-and-beveling machine. To find equipment that is actually usable and available in Bangalore Division, you need to define the finished weld-end geometry, workpiece range, material, tooling and delivery status before comparing quotations.
Key takeaways
- Define the weld joint’s bevel angle, root face, root gap, and tolerance first.
- Match machine capacity to tube diameter, wall thickness, length, and material.
- Request tool specifications for stainless steel, carbon steel, and alloy workpieces.
- Use production workpieces for supplier trials, acceptance testing, and installation planning.
Define the Edge Preparation Your Welding Process Requires
Define the weld joint before selecting a machine. It may require a square face, a root face, a root land, or a specified bevel angle and root gap. The machine must remove burrs, cut the bevel, face the end square to the tube axis, and leave a consistent weld-ready land.
| Process | Required result | Do not confuse it with |
|---|---|---|
| Deburring | Removes raised metal and sharp burrs | It does not create a weld groove |
| Chamfering | Creates a small angled edge for handling or assembly | It is not automatically a weld bevel |
| Facing | Makes the tube end square to its axis | It does not set groove angle or root gap |
| Countersinking | Enlarges the bore entrance with a tapered recess | It is not external beveling |
| Weld beveling | Forms the specified groove angle, root face and land | It requires the welding procedure’s dimensions |
Treat edge preparation machine as an umbrella: stationary pipe bevelers, portable OD-mounted bevelers, ID-clamping machines, tube end facers, chamfering machines, and facing-and-beveling units do different work. Specify the result, not merely the category. Cold machining avoids slag, oxide, and a thermal-cutting heat-affected zone. Include angle, land width, root face, concentricity, and tolerance in the quote.
Industrial edge preparation equipment and a metal edge preparation machine must be judged against those requirements, not a catalogue label alone.
Match the Machine Category to Your Pipe or Tube Dimensions
A machine fits your workpiece only when its OD, ID, wall-thickness and length limits overlap the complete production range. A listing for pipe edge preparation machinery does not prove suitability for every tube geometry: stationary bevelers, portable OD-mounted bevelers, ID-clamping machines, tube end facers and combined facing-and-beveling units impose different constraints.
| Machine category | Capacity details to verify | Main limitation |
|---|---|---|
| Stationary pipe beveler | Outside diameter, wall-thickness range, maximum length and workpiece weight | The chuck or tooling may not accept small-bore or unusually long pipe |
| Portable OD-mounted beveler | OD range, minimum wall thickness, available clearance and motor capacity | External cutting forces can collapse thin-wall tube |
| ID-clamping machine | Usable tube ID, mandrel range, minimum straight length and end access | It cannot enter lined, scaled, closed-end or very small bores |
| Tube facer or chamfering machine | Tube OD, ID, wall thickness, collet size and end-length tolerance | Nominal pipe capacity does not establish thin-tube support or repeatability |
Check the minimum straight length from the tube end to the first bend, collar or obstruction. Confirm the maximum workpiece length and allowable material weight; a machine that accepts the diameter can still be unsafe or impossible to load.
- Give the supplier the actual OD, ID, wall-thickness range, material hardness and required pieces per hour.
- State whether you need a weld bevel, square facing, deburring or a simple chamfer.
- Require the quoted metal edge preparation machine to identify tooling, feed control, burr limit and power supply.
Specify Materials, Edge Profiles and Cutting Tools Before You Compare Quotes
A meaningful quote starts with the workpiece, not the machine name. State the material grade, hardness range, OD, ID, wall thickness, minimum straight length, maximum length, and piece weight. Add the required production rate, allowable burr, surface-finish limit, power supply, and whether the operation is shop-based or field-based.
Give the supplier this tooling information:
- Profile: bevel angle, land width, root face, corner radius, and whether the end must be faced square to the tube axis.
- Cutting method: cold machining, carbide inserts, HSS cutters, or another specified tool system.
- Tooling: insert grade and coating, nose radius, cutter diameter, holder type, pilot, mandrel, collet, or ID-support arrangement.
- Material condition: mill scale, oxide, existing thermal-cut edge, coating, and whether a heat-affected zone must be removed.
- Hydraulic interface: required pressure and flow, motor type, filtration, hose connections, and duty cycle if using a hydraulic power pack.
| Edge result | What to specify | Tooling or machine consequence |
|---|---|---|
| Weld bevel | Angle, land, root-face tolerance, and surface condition | Bevel cutter with controlled axial and radial adjustment |
| Square-faced end | Squareness tolerance and allowable face runout | Facing cutter with firm OD, ID, mandrel, or collet support |
| Simple chamfer | Angle, width, and burr limit | Chamfer cutter; it is not evidence of weld-bevel capability |
ISO 9692-1 can describe a welding joint preparation, but it does not prove machine capacity or accuracy. Ask for a drawing and measured sample result before comparing pipe edge preparation machinery or other industrial edge preparation equipment quotes.
Check Actual Edge Preparation Machine Availability in Bangalore Division
A catalogue page does not prove edge preparation machine availability in Bangalore Division. Before treating a listing as ready equipment, ask the edge preparation machine supplier Bangalore for a dated stock confirmation naming the exact machine type, model, serial number, outside-diameter and wall-thickness range, and current location.
1. Request photographs or a live video showing the machine, nameplate, control panel, tooling, and serial number. A generic product photograph is not stock evidence.
2. Ask for a written dispatch date, demonstration date, included tooling, spare cutting tools, commissioning scope, and service response time. “Available” without these details often means the supplier can order it.
3. Check whether the quoted machine is a stationary pipe beveler, portable OD-mounted beveler, ID-clamping unit, tube end facer, or combined facing-and-beveling machine. One category will not automatically process your tube geometry.
| Supplier statement | What it proves | What you still need |
|---|---|---|
| Ex-stock | A named unit is physically held | Serial-number evidence, inspection access, dispatch commitment |
| Made to order | Production begins after your order | Manufacturing lead time, drawing approval date, delivery milestone |
| Catalogue listing | The product exists in the supplier’s range | Stock location, exact capacity, tooling, and committed lead time |
For installation, obtain the required phase, frequency, connected load, hydraulic-oil specification, lifting method, floor requirements, and operator-training scope in the quotation. Hydropower Engineers should be assessed by the same written evidence, not by catalogue presence alone. A demonstration using your diameter, wall thickness, bore access, and material exposes unavailable tooling before payment.
Related product
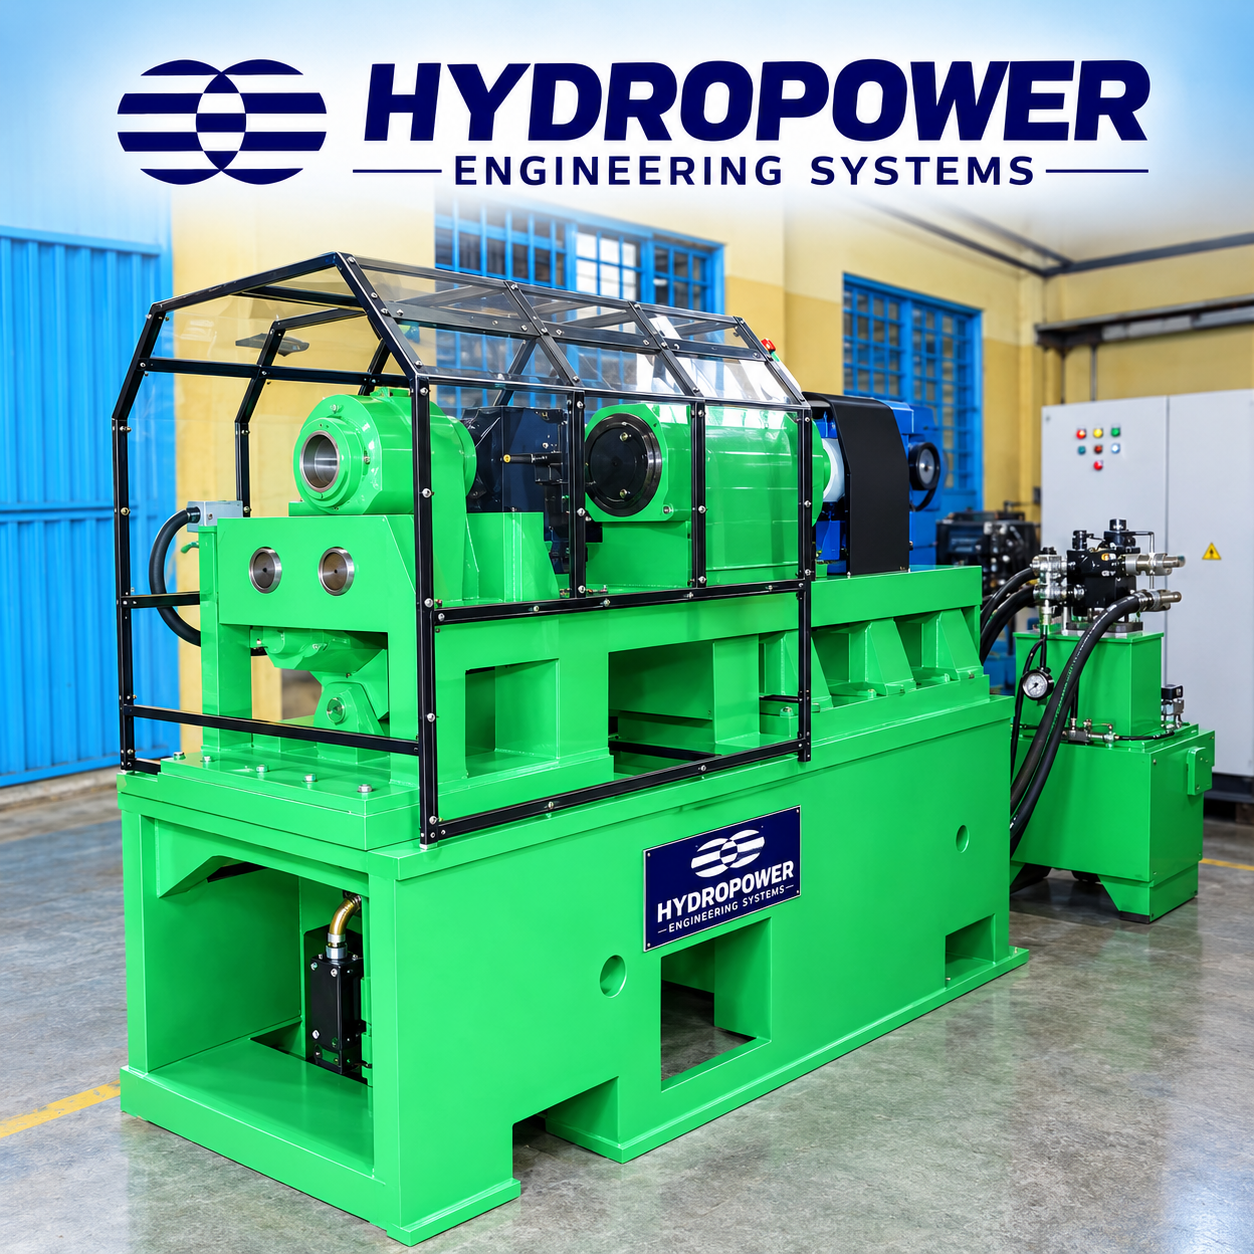 | Edge Preparation Machine Hydropower Engineering Systems offers a robust and precision-engineered Pipe Chamfering Machine / Edge Preparation Machine, developed for efficient... View product → |
Use Your Own Workpieces for Acceptance and Installation Planning
A supplier demonstration proves little unless it uses your representative workpieces. Ask an edge preparation machine supplier Bangalore to run the actual material, outside diameter, wall thickness, profile, batch quantity and tooling specified for production.
1. Submit sample workpieces before ordering. Record bevel angle, land width, end squareness, concentricity, surface finish and repeatability across a production-sized batch. Check chip evacuation, tool wear and cycle time, not just the first acceptable cut.
2. Match the demonstration machine to the quoted model and configuration. Industrial edge preparation equipment includes stationary pipe bevelers, portable OD-mounted machines, ID-clamping units, tube end facers and combined facing-and-beveling machines. A pipe beveler listing does not prove suitability for thin-wall tubes, mandrels or collet tooling.
3. Put acceptance limits in the purchase order. State measurement methods, permitted tolerances, material grade, tool type, wall thickness and the remedy for failure. ISO 9692-1 can guide steel joint preparation, but it does not establish machine capacity or accuracy.
4. Require a commissioning sheet covering phase, voltage, frequency, connected load, hydraulic-oil specification, lifting method, floor or foundation needs, ambient limits and operator training. Specify hydraulic cleanliness using the machine supplier’s required ISO 4406 code; do not infer it from pressure rating.
5. Obtain a production-readiness date tied to installation, utilities, trial parts, training, spares and final acceptance. Treat a catalogue listing or “available” claim as unverified until the demonstration, delivery lead time and installation scope are documented.
Frequently asked questions
What edge preparation does a welding process require?
Specify whether the joint needs a square face, root face, root land, bevel angle, and root gap before selecting equipment. The machine must produce those features within your welding procedure’s tolerances.
How do you match an edge preparation machine to a pipe or tube?
Compare the machine’s diameter range, maximum wall thickness, workpiece length, clamping method, spindle speed, and tooling with your actual pipe or tube dimensions.
What information should you provide when requesting an edge preparation machine quote?
Provide material grades, outside and inside diameters, wall thicknesses, required edge profiles, production volumes, dimensional tolerances, and the cutting tools required.
How can you verify edge preparation machine availability in Bangalore Division?
Ask suppliers for current lead time, machine location, demonstration access, tooling stock, installation scope, service coverage, and a trial using your own workpieces.